
Metalworking
Metalworking fluids
Metal cutting soluble fluids
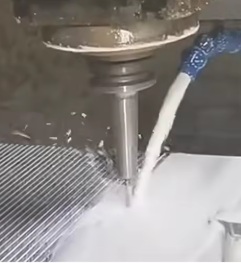
Industrial soluble metalworking fluids (MWFs), often called soluble oils or emulsions, are concentrated lubricants designed to be mixed with water for cooling and lubricating metal parts during cutting, grinding, and machining. They provide high-performance cooling for high-speed operations while minimizing rust and improving surface finishes on metals like aluminium, steel, and ferrous alloys.
Metalworking fluids (also referred to as coolants or lubricants) are engineered liquids applied to the interface between the cutting tool and the workpiece. At the point of contact, extreme pressure and friction generate intense thermal energy that threatens tool geometry and part dimensions.
Metal machining soluble emulsion
Soluble oils are emulsions that mix oil with water, typically containing 30% to 85% oil along with emulsifiers.
- Semi-synthetics combine a lower oil content, typically 5% to 30% oil, with synthetic additives to improve performance across a range of cutting conditions.
- Synthetic fluids contain 0% petroleum oil. They are formulated from chemical compounds designed for maximum cooling and cleanliness.
| PRODUCT | Mineral oil content | Metals | Application | |
| CutFluid ME 9810 | 20 | cast iron and aluminium alloys | Universal metalworking fluid for all chipforming processes, designed for use at 4 – 15 % |  |
| CutFluid ME 3580 | 80 | cast iron, aluminium and copper alloys | For all chip forming processes, designed for use at 6 to 15 % | |
| CutFluid ME 1790 | 40 | cast iron, aluminium and other non-ferrous metals | For all chipforming processes, designed for use from 4.0 % | |
| CutFluid ME 4260 | 30 | cast iron, aluminium and other non-ferrous metals | for all chip forming processes, designed for use from 5.0 % | |
Grinding Fluids
| PRODUCT | Mineral oil content | Metals | Application | |
| GrindFluid MS 2042 | Free | steel | Grinding processes, designed for use at 4 – 5 % | |
| GrindFluid MS 05155 | Free | tungsten carbide materials and tungsten carbide tools. Also for grinding on ferrous materials | Grinding with tungsten carbide tools, designed for use at 5 to 6 % | |
| GrindFluid S 1931 | Free | cast iron and steel | Universal grinding fluid, designed for use at 4 – 10 % | |
Thread cutting oils
| PRODUCT | Viscosity at 40 °C | Metals | Application | |
| Molylub Thread 3300 | 24 | all kinds of steel, aluminium | for thread operations (e. g. thread cutting, thread rolling and thread tapping) as well as for deep whole drilling | |
| Supercut AL | 20 | Specially for aluminium | For thread cutting, difficult machining | |
Fully synthetic MWFs are typically true solutions that contain no oil or emulsifiers. In the case of fully synthetic metalworking fluids, lubricity is provided by water soluble – mostly polyalkylimide glycol-based – lubricants.
Synthetic metalworking grinding fluid
In terms of performance, the fully synthetic MWFs can have certain limits when compared with the emulsion-type fluids. However, thanks to the fact that they do not contain emulsifiers or mineral oil, they generate various other additional benefits:
- Comparably easy to formulate
- Lower complexity (fewer components required)
- Advanced tramp oil rejection
- Typical low foaming behaviour
- Increased bio-resistance (may require less biocide)
- Better visibility of operations
In recent years, the use of high lubricity fully synthetic fluids for aluminium machining has increased, and this is why performance additives are more frequently requested for this purpose.
Emulsion type Molylub CutFluid H Extra
Emulsion-type metalworking fluids (MWFs) mostly contain mineral or vegetable-based oil which is emulsified with the aid of different types of non-ionic and anionic emulsifiers.
Emulsion-type MWFs are still the main type of water-miscible fluids used, because they offer excellent lubricity and cooling, making it possible to machine most metals even in heavier and more difficult operations.